Industrial Steel Drive In Pallet Rack
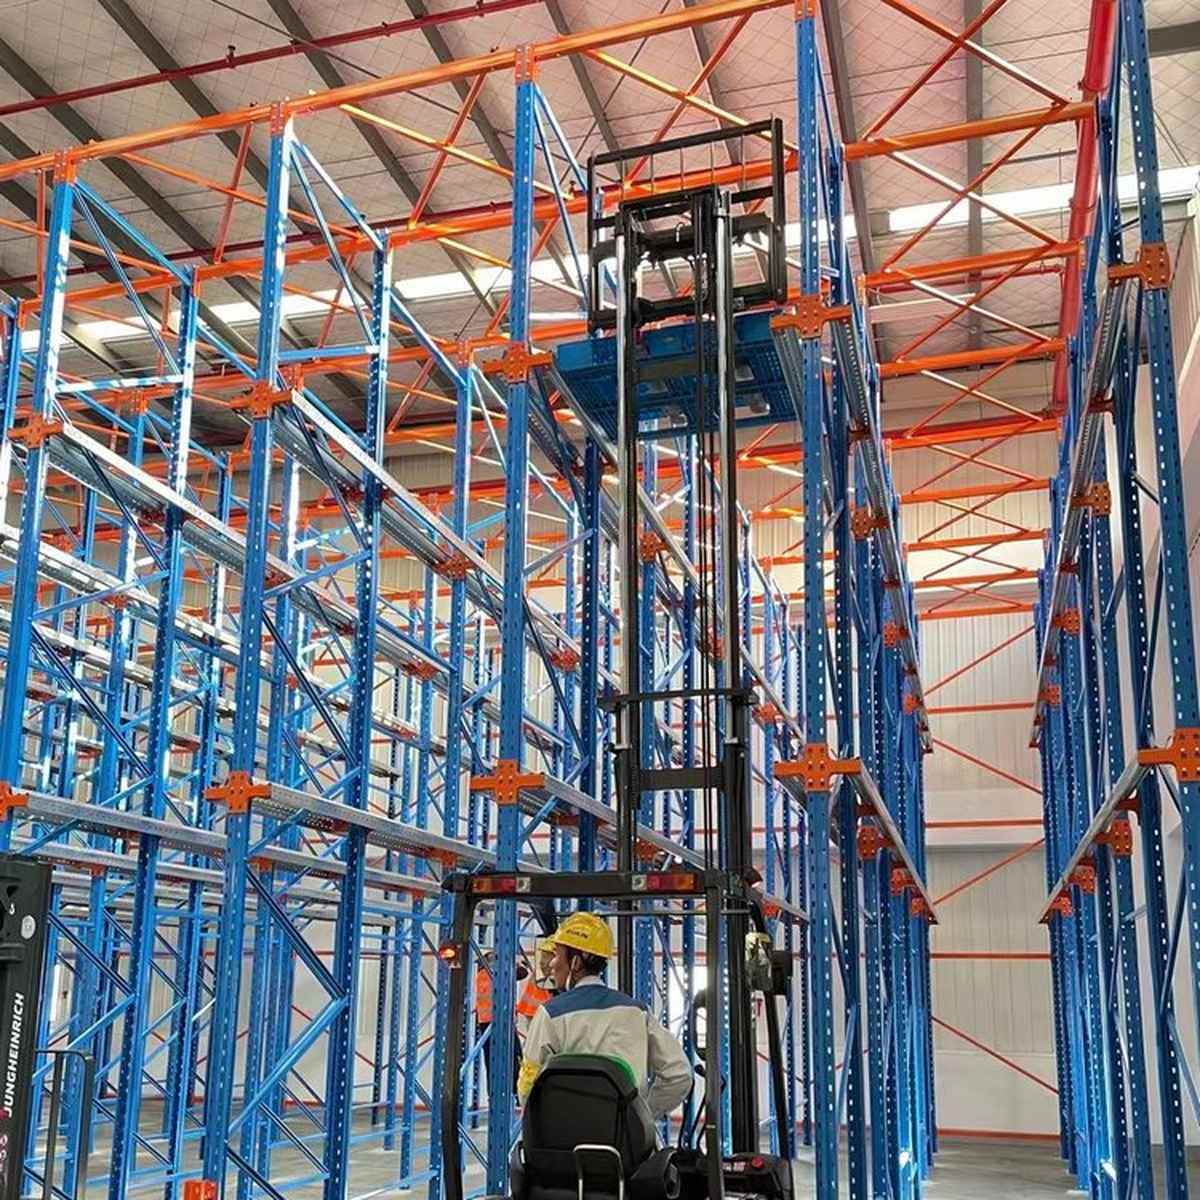
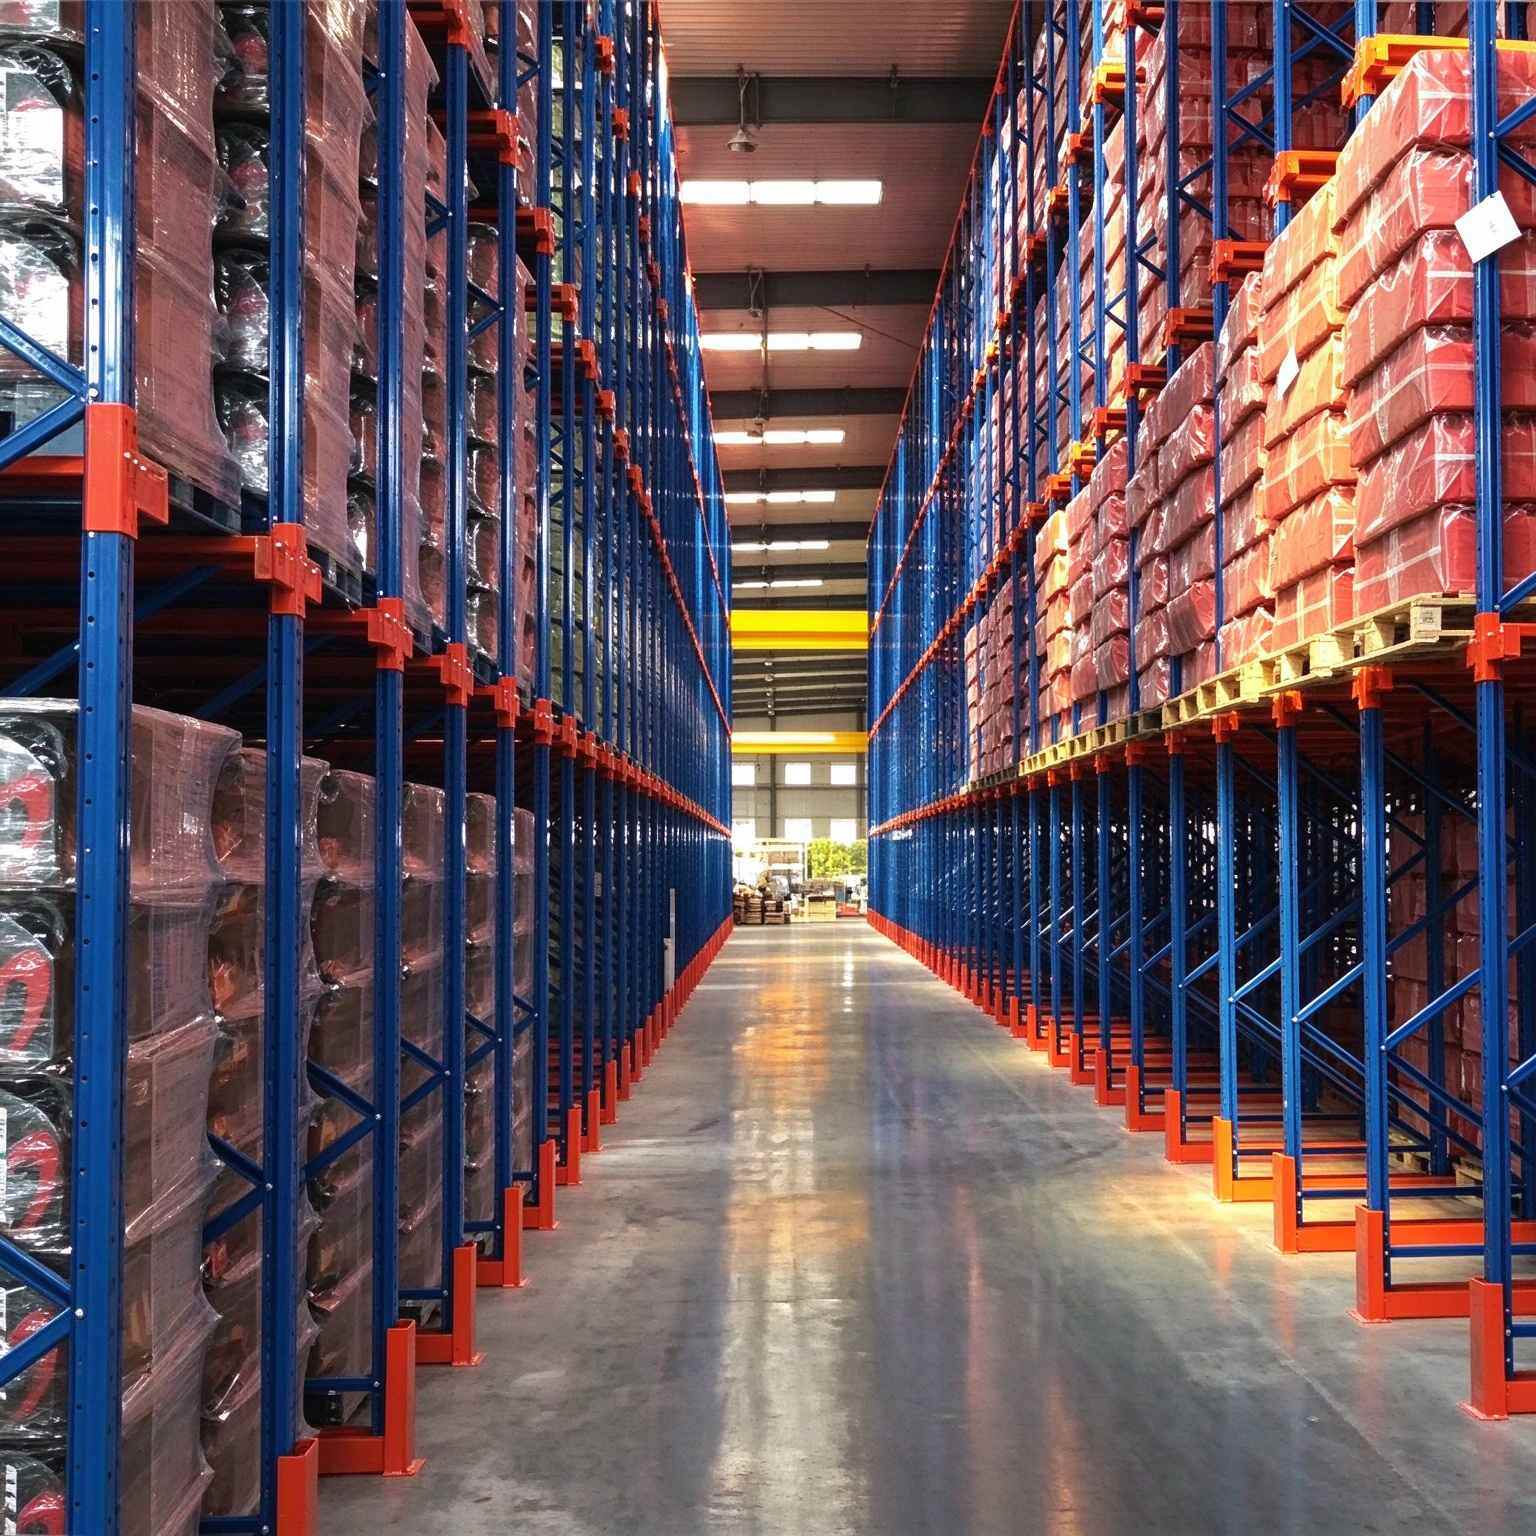
Industrial steel drive in pallet rack is a high-density pallet storage solution designed to eliminate redundant forklift aisles and optimize warehouse footprint. Forklifts can drive directly inside the rack lanes to load and unload pallets from the front of the system, enabling continuous stacking of pallets deep within the rack structure.
- ✔ High space utilization — increases capacity by over 30%
- ✔ LIFO storage for batch-managed goods
- ✔ Robust integrated steel structure
- ✔ Custom dimensions for pallet size & layout
Industrial steel drive in pallet rack-Features
- ✔ High Space Utilization: Eliminates separate aisles. Storage capacity can increase by over 30% compared with standard pallet racking.
- ✔ LIFO Storage Principle: Last-In, First-Out system for each lane, ideal for batch-managed goods without strict expiry control.
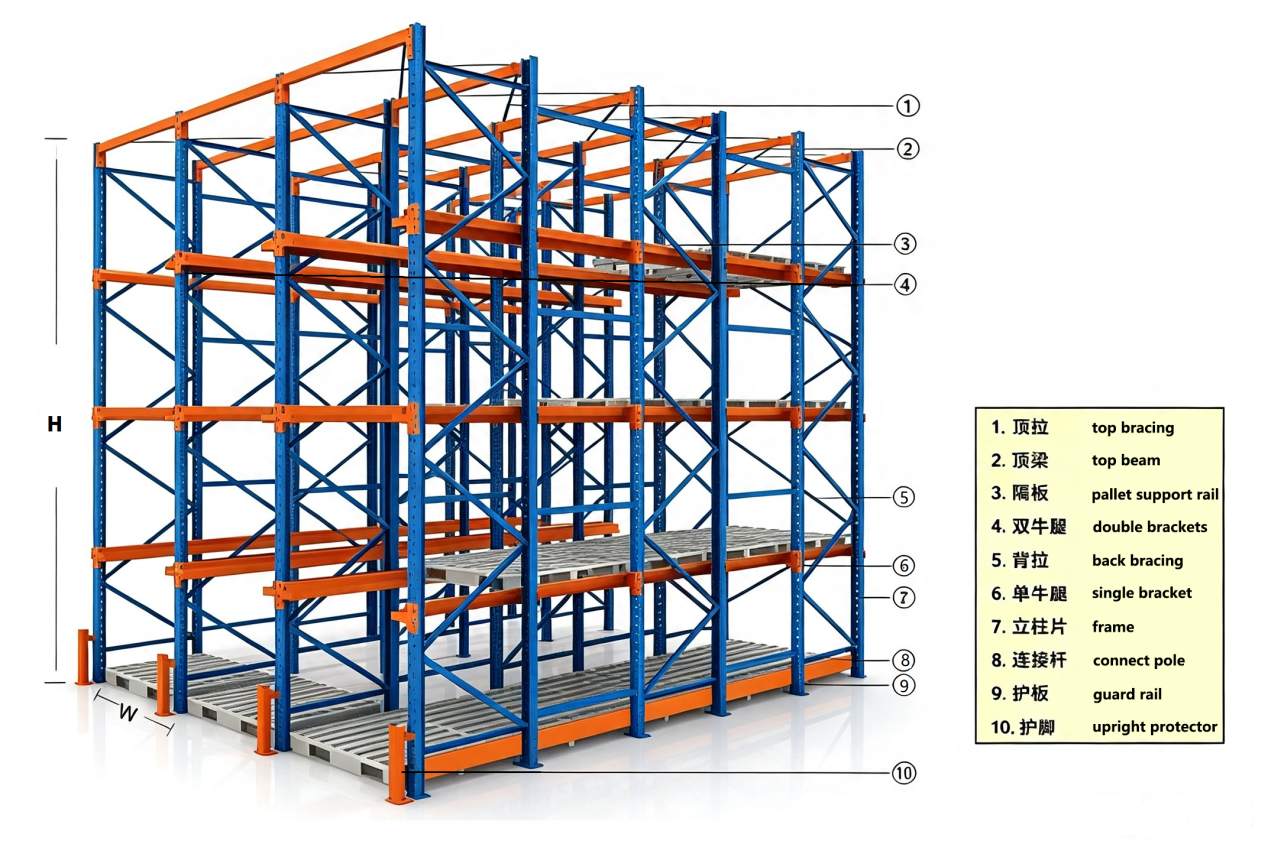
- ✔ Robust Integrated Structure: Consists of uprights, top beams, brackets and support rails. Heavy load capacity and strong impact resistance.
- ✔ Custom Dimensions: Lane depth, height and beam levels can be customized according to pallet size and warehouse layout.
- ✔ Anti-corrosion Surface Finish: Powder coating for rust and wear resistance, suitable for ambient warehouses and cold rooms.
- ✔ Lower Infrastructure Cost: Fewer forklift aisles required, saving investment on warehouse construction and lighting.
Industrial steel drive in Standard Specifications
- ✔ Rack Height: Standard 3–10m, customized according to warehouse ceiling height.
- ✔ Load per pallet: Standard 1000kg–1500kg per pallet position.
- ✔ Lane depth: Normally 2–6 pallets deep for one-way LIFO design.
- ✔ Compatible pallets: Standard 1200×1000mm, 1200×800mm Euro pallet, 1100×1100mm.
- ✔ Adjustment pitch: 75mm hole pitch for flexible layer height adjustment.
- ✔ Material: Q235 steel, electrostatic powder coating, coating thickness 60–80μm.
Industrial steel drive in-Application
- ✔ Food & Beverage Industry: Mass storage of packaged goods, raw materials and finished products in cold storage.
- ✔ Cold & Freezer Warehouses: Minimize aisle space to get the most of expensive cold room volume.
- ✔ Manufacturing Finished Goods Warehouse: Bulk palletized storage of factory raw materials and finished products.
- ✔ Bulk Commodity Storage: Chemical materials, paper rolls, building materials and other large-volume uniform goods.
- ✔ 3PL Logistics Centers: Seasonal stock and bulk pallet cargo transit.
Drive In Racking System- Component